
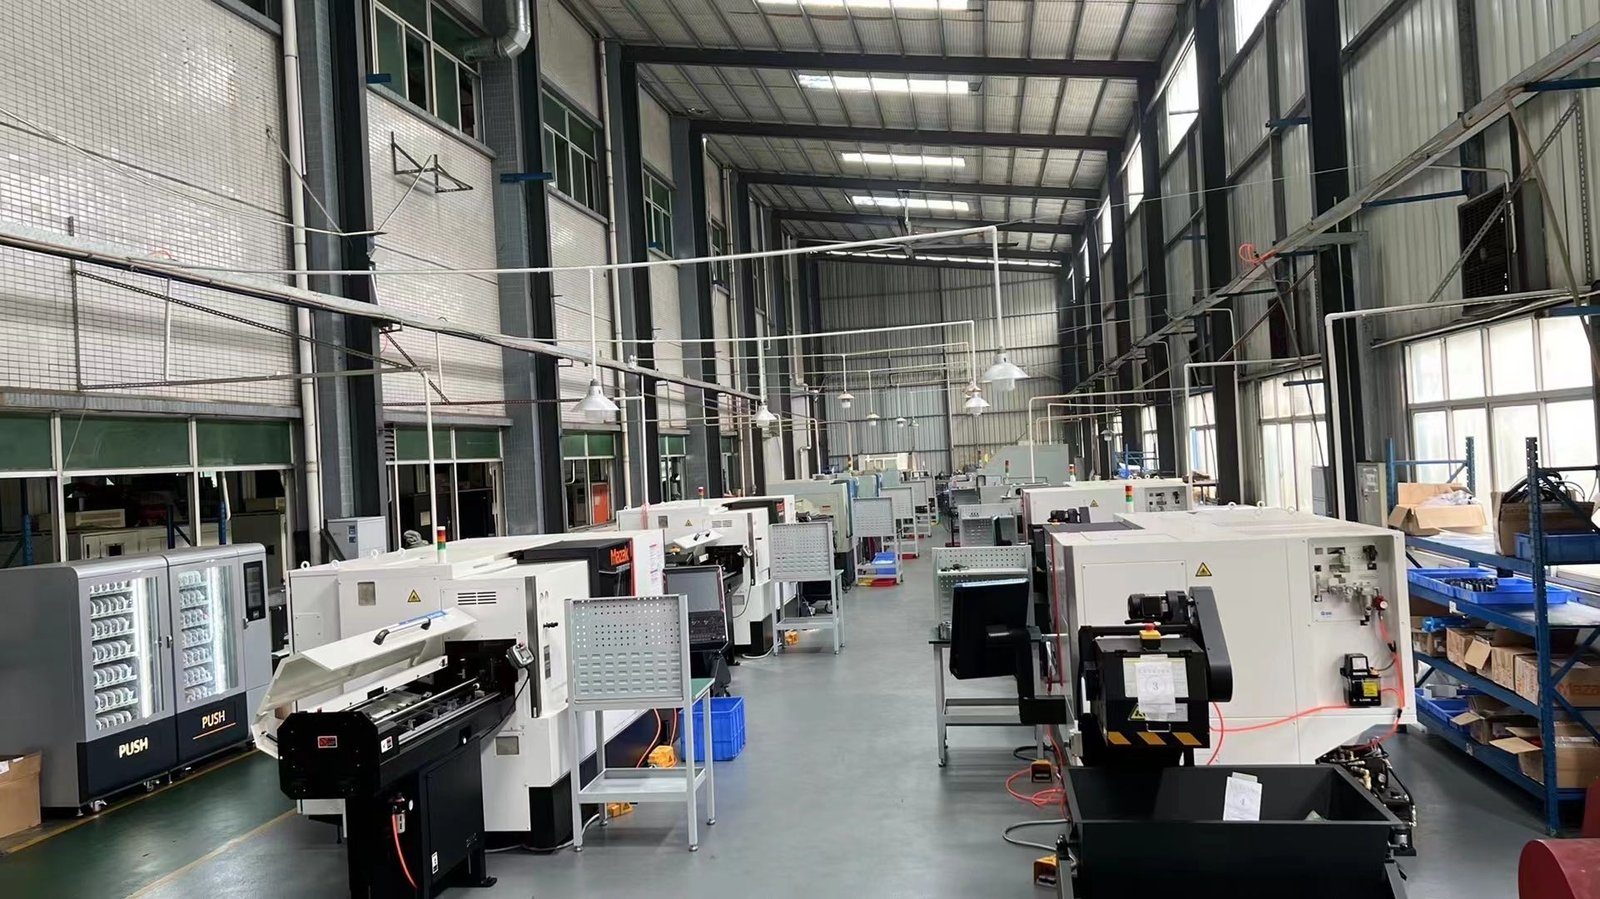
- 6,800 m² across two buildings in Hengli Town, Dongguan — production, inspection, and engineering under one roof.
- ISO 9001:2015 / IATF 16949:2016 / ISO 14001:2015 — certificate numbers published and verifiable.
- Wrought stock versus build-dependent microstructure — the first dividing line.
- On this page the focus is leadtime: where the two processes actually separate.
- The two cost curves cross; the crossover quantity is the real question.
Which one is actually faster?
Lead time is not cycle time. A machined part's lead time is mostly queue position, fixture design, and first-article inspection; its actual cutting time may be an hour. A printed part's lead time is mostly build time and post-processing, with no fixture to design.
That is why printing often wins at quantity one and loses at quantity twenty: the machined part's fixed costs are front-loaded, so the first one is slow and the next twenty are not. Asking for both numbers separately, first-article lead and repeat lead — is what makes the comparison honest.
The schedule risk differs too. A machined part competes for machine time; a printed part competes for build chamber time. Which queue is shorter is a property of the supplier's load, not of the process.
What design decisions move the cost on CNC turning service?
Three design decisions drive most of the cost on a machined part: internal corner radii matched to a real cutter diameter, cavity depth kept within about four times the tool diameter, and a general tolerance on every feature that does not mate. Each one changes the tool that can be used, and the tool determines how much material can be removed per minute, which is why these matter more than any process selection.
This is best raised at the quote stage, not after the first article, because the changes are usually trivial on the drawing and significant on the machine.
How much capacity sits behind it?
more than 100 machines with depth in every relevant family — 50+ three-axis, 20+ four-axis, 20+ five-axis, 25+ turning centres, plus Swiss-type, grinding, and wire EDM.
Which certifications apply, and what do they exclude?
Three certificates, each with a number you can check with the registrar:
| Standard | Certificate number | Scope note |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Quality management system |
| IATF 16949:2016 | 131941/A/0001/SM/En | Automotive QMS — excludes clause 8.3 product design |
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management system |
The IATF 16949 certificate excludes clause 8.3 (product design). That is normal for a build-to-print manufacturer and it is stated here rather than left for an auditor to discover: we cut to the drawings you provide, it does not originate the design.
The crossover quantity, and what moves it
Machining carries a fixed cost, programming, fixturing, first-article inspection, and a low variable cost per part. Additive carries almost no fixed cost and a high, roughly flat cost per part. The two lines cross somewhere, and the crossing point is what determines the right process.
Below the crossover, printing is cheaper. Above it, machining is. The crossover quantity is not a constant: it moves with part size, material, and tolerance, which is why the useful question is not which is cheaper but at what quantity this part crosses over.
The mistake that costs money is comparing a printed prototype price to a machined production price. Those are two different points on two different curves, and the comparison says nothing about either process.
Where the crossover quantity sits
Machining carries a fixed cost — programming, fixturing, first-article inspection, and a low variable cost per part. Additive carries almost no fixed cost and a high, roughly flat cost per part. The two lines cross somewhere, and the crossing point is what determines the right process.
Below the crossover, printing is cheaper. Above it, machining is. The crossover quantity is not a constant — it moves with part size, material, and tolerance — which is why the useful question is not "which is cheaper" but "at what quantity does this part cross over".
| Factor | Cnc Turning Service | Additive manufacturing |
|---|---|---|
| Material properties | Wrought stock, certifiable to standard | Build-dependent, often anisotropic |
| Typical tolerance±0.002 mm (turning) / ±0.003 mm (milling) | Looser; interfaces usually machined | |
| Fixed cost | Programming, fixturing, FAIR | Near zero |
| Variable cost per part | Low and falling with volume | High and roughly flat |
| Geometry freedom | Limited by tool access | Internal channels and lattices possible |
| Lead time at qty 1 | Fixture and programme dependent | Often shorter |
| Best quantity band | Prototype through production | One-offs and geometry validation |
The practical test: if the part has a datum structure that has to hold a geometric relationship, machining is usually the answer. If the part's value is in a shape no cutter can reach, printing is.
Using both processes on one part
Yes, and it is often the right answer for a complex, low-volume, tight-interface part: print the near-net shape, then machine the datums, sealing faces, and threaded features. The print buys geometry the cutter cannot reach; the machining buys the tolerance the print cannot hold.
The cost of that route is two processes and a handover between them, so it earns its keep only where the geometry genuinely cannot be cut. Where it can be cut, cutting it is simpler and cheaper.
What tolerance applies?
±0.003 mm on CNC milling, ±0.002 mm on CNC turning; ±0.002 mm where precision grinding or wire EDM is used, set feature by feature when we quote.
Which legal entity is actually responsible for the work?
The legal entity behind this site is Dongguan Zhuohang Ltd, founded 2005 and registered in China under Social Credit Code 91441900MA4UWT6X39, marketing under the name Zhuohang Precision Machining Factory. Its registered and production address is No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470.
Use the National Enterprise Credit Information Publicity System and the 18-character code to verify a Chinese manufacturer. Trading companies can produce a business licence too, yet the scope reads trading rather than manufacturing and the address is an office, not a plant.
What this shop actually runs
If you ask for capability evidence, you deserve a specific answer. This facility operates 100+ CNC machines across 6,800 m2 in Dongguan, China, staffed by 100+ people. The machines, listed by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Set up for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Set up for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Set up for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Set up for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Set up for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance bands: ±0.003 mm milled, ±0.002 mm turned, ±0.002 mm ground or wire-cut. Capability indices: Ppk >= 1.67 at the initial study; Cpk >= 1.33 ongoing in production.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En) · IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded) · ISO 14001:2015 (116024/B/0001/UK/En), held by Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, since 2005).
Service area: we supply Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, with worldwide delivery from China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Not sure this is the right process?
Send the model and the drawing and get a straight answer on whether this route is the right one, including where a design change would cut cost. Reach Felipe Iglesias at [email protected] or +86 13126536955.
Frequently Asked Questions
Which markets do you export to?
In short, Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa. Our service area also spans Europe, the Americas, Asia, Oceania and Africa — based in China, we serve customers worldwide.
What happens if the first article does not conform?
In short, The nonconformance is documented and the corrective action is agreed before any further parts are made. Whether the replacement cost sits with the plant or the customer depends on where the deviation came from, so the revision and the drawing standard are confirmed in writing at the start.
Is 3D printing cheaper than CNC machining?
At quantity one, sometimes. Above the crossover quantity — which depends on size, material, and tolerance — machining is cheaper, and the gap widens with volume. A printed part that needs its interfaces machined carries both costs.
What is the difference between a prototype build and a production build here?
Usually only quantity and scheduling. Both run on the same machines and the same process, which is what makes a later ramp a scheduling change rather than a re-qualification.
What tolerances can you hold?
In short, ±0.003 mm on CNC milling, ±0.002 mm on CNC turning, and ±0.002 mm where precision grinding or wire EDM is used. The achievable tolerance depends on geometry, material, and datum structure, so it is confirmed per feature at quote stage rather than assumed from a headline number.
Can a printed part be machined afterwards?
Yes, and it frequently is. Sealing faces, bearing seats, and threaded features are machined on printed parts as a matter of course when they have to hold a tolerance or a fit.
Do you sign NDAs before reviewing drawings?
Yes. Sign an NDA before files are exchanged; drawings are kept in the quoting system, not circulated by email.
Continue reading: 3 Axis CNC Turning Service · 4 Axis CNC Turning Service · 5 Axis CNC Turning Service
Standards referenced on this page
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ISO 14001 — Environmental management systems — Requirements with guidance for use
- IATF 16949:2016 — Automotive quality management system standard