
- ISO 9001:2015 / IATF 16949:2016 / ISO 14001:2015, certificate numbers published and verifiable.
- Manufacturing to your print: the plant cuts to your design and reports against your drawing.
- Aluminum: Aluminium is the forgiving end of the spectrum: it cuts fast, conducts heat away from the edge, and is easy on tools.
- Grades in regular use: 6061-T6 for general work and anodising, 7075-T6 for strength, 6082 for structural use in Europe, 2024 where fatigue matters.
- Incoming stock is verified against the mill certificate before it is cut.
Why aluminum needs its own process
Aluminium is the forgiving end of the spectrum: it cuts fast, conducts heat away from the edge, and is easy on tools. The problems are different — built-up edge at low speed, chip evacuation in deep pockets, and the fact that a fast cycle time makes the setup time a larger fraction of the cost, so batch size dominates price.
Cast plate and wrought bar behave differently under stress relief and can move differently after machining — worth stating on the drawing.
What finishing and surface treatment apply to aluminum?
Anodising (Type II and Type III hardcoat), chem film, and powder coat are all routine. Type II adds roughly 5–15 µm per surface, which must be allowed for on threaded and press-fit features.
You specify finishing on the drawing, not assume it at the end. Where a coating adds thickness, threaded and press-fit features need the allowance stated, because a coating applied after inspection changes the fit.
Why aluminum costs what it costs to cut
The problems are different — built-up edge at low speed, chip evacuation in deep pockets, and the fact that a fast cycle time makes the setup time a larger fraction of the cost, so batch size dominates price.
The lever that matters most for you is usually design rather than process: pocket depth, corner radius, and wall thickness change cycle time more than any tooling choice, because they determine the tool that can be used and therefore how much material can be removed per minute.
Three things that change the price without changing the part
Aluminium cuts fast, so setup time becomes a larger share of the cost and batch size dominates the unit price. The design levers are chip evacuation in deep pockets and wall stability, a 1 mm wall on a large pocket will move under cutting pressure even in aluminium, and holding it flat costs a slower finishing pass.
This should come up when quoting, before any metal is cut, because the changes are usually trivial on the drawing and significant on the machine.
Which standards the plant is certified to
Three certificates, each with a number you can check with the registrar: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En).
The IATF 16949 certificate excludes clause 8.3 (product design). That is normal for a build-to-print manufacturer and it is stated here rather than left for an auditor to discover: the plant manufactures to your design, it does not originate the design.
What tolerance applies?
±0.003 mm on CNC milling, ±0.002 mm on CNC turning; ±0.002 mm where precision grinding or wire EDM is used, set feature by feature when we quote.
Choosing a grade within aluminum
6061-t6, 7075-t6, 6082, 2024, and cast plate grades are the grades that come up in practice. 6061-T6 for general work and anodising, 7075-T6 for strength, 6082 for structural use in Europe, 2024 where fatigue matters.
Your grade selection is usually settled by the service environment — corrosion, strength, or temperature, and only then by machinability. If you choose on machinability first, your part meets the drawing and fails in service.
What happens to tolerance on aluminum?
High thermal expansion means a part measured warm will measure differently when cool. On a tight-tolerance part the finishing pass is taken after the part has returned to ambient, and the measurement is taken at 20 °C.
The general rule for your part is that a tolerance is held by the process, not by the machine. Where a feature is tight, the finishing pass is separated from roughing, the part is allowed to stabilise, and the measurement is taken at a controlled temperature.
What identifies the legal entity behind the machines?
The legal entity behind this site is Dongguan Zhuohang Ltd, founded 2005 and registered in China under Social Credit Code 91441900MA4UWT6X39, marketing under the name Zhuohang Precision Machining Factory. Its registered and production address is No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470.
Use the National Enterprise Credit Information Publicity System and the 18-character code to verify a Chinese manufacturer. Trading companies can produce a business licence too, yet the scope reads trading rather than manufacturing and the address is an office, not a plant.
How much capacity sits behind it?
over a hundred machines with depth in every relevant family. 50+ three-axis, 20+ four-axis, 20+ five-axis, 25+ turning centres, plus Swiss-type, grinding, and wire EDM.
Why the material decision comes first
On a CNC turning service part, the material is the single biggest lever on the price, the tolerance and the lead time, so it should be decided before the drawing is frozen. Aluminium machines fast and cheap and suits light, non-structural parts. Steel and stainless add strength and corrosion resistance at a higher machine cost. Titanium and Inconel hold high-temperature strength but run many times slower and wear tooling fast. If you pick the material for the service - the load, the environment, the temperature - you get a part that works and a quote that is honest, instead of paying for an alloy the part never needed.
Specifying the grade, not just the name
The material name is not enough; the grade is the specification. Aluminium 6061-T6 and 7075-T6 are different strengths, and stainless 303 and 316 are different jobs. The grade, the temper and the condition all belong on the drawing, and the mill certificate confirms them. Incoming stock here is verified against the mill certificate before it is cut - composition by XRF, hardness where specified. Contact Felipe Iglesias at [email protected] or +86 13126536955 with the material and the grade, and the quote reflects the real stock.
The evidence behind the numbers
Ask for proof and the answer is specific: Dongguan Zhuohang Ltd runs 100+ CNC machines on a 6,800 m² floor in Hengli Town, Dongguan, including the Mazak VARIAXIS I-600 five-axis, the INTEGREX I-250H S mill-turn, Brother SPEEDIO, and TSUGAMI, STAR and CITIZEN Swiss lathes. Inspection runs on a Hexagon CMM with the 10:1 gauge rule, and ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015 are held by verifiable certificate number. Critical characteristics are tracked with Ppk 1.67 initial and Cpk 1.33 in production - a tolerance quoted here is a tolerance held.
Buyers across Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa are served from Dongguan with worldwide shipping. MOQ is 1 piece; lead times run about 3 / 7 / 30 days. Send the drawing and quantity to Felipe Iglesias at [email protected] or +86 13126536955 and the quote returns with the process spelled out.
Starting your order
The quickest route to a part is a model and a quantity. Send the STEP or IGES file with a 2D drawing that names the tolerances, datums, material grade and finish, plus the quantity and the lead time you need, and you get an itemised quote - material, setup, cycle time and inspection - not a round figure. No finished drawing? Send what you have and the questions that are blocking you; the goal is to begin, not to wait for a flawless package.
Email Felipe Iglesias at [email protected] or call +86 13126536955. MOQ is 1 piece, lead times run roughly 3 / 7 / 30 days, and shipping covers Europe, the Americas, Asia, Oceania and Africa, plus worldwide from Dongguan.
The tolerance and finish numbers
On this floor milling holds ±0.003 mm, turning ±0.002 mm, and grinding or wire EDM ±0.002 mm, verified on a Hexagon CMM against the drawing datums. As-milled surfaces run Ra 0.8 to 3.2 µm, ground Ra 0.2 to 0.4 µm, polished Ra 0.05 to 0.1 µm. Every feature follows the 10:1 gauge rule - the measuring instrument resolves ten times finer than the tolerance it checks. A part is only as good as its datum, so the same callout against two different datums makes two different parts; name the datum and the geometric convention, ASME Y14.5 or ISO.
De-risking a first order
A trial order of a few pieces is the cheapest insurance you can buy — it proves the routing, the tolerance and the paper trail on a small batch before the volume order locks in. One floor, one quality system, one accountable party, whether the run is a single part or a full production lot, so what the trial confirms is what production repeats.
What this shop actually runs
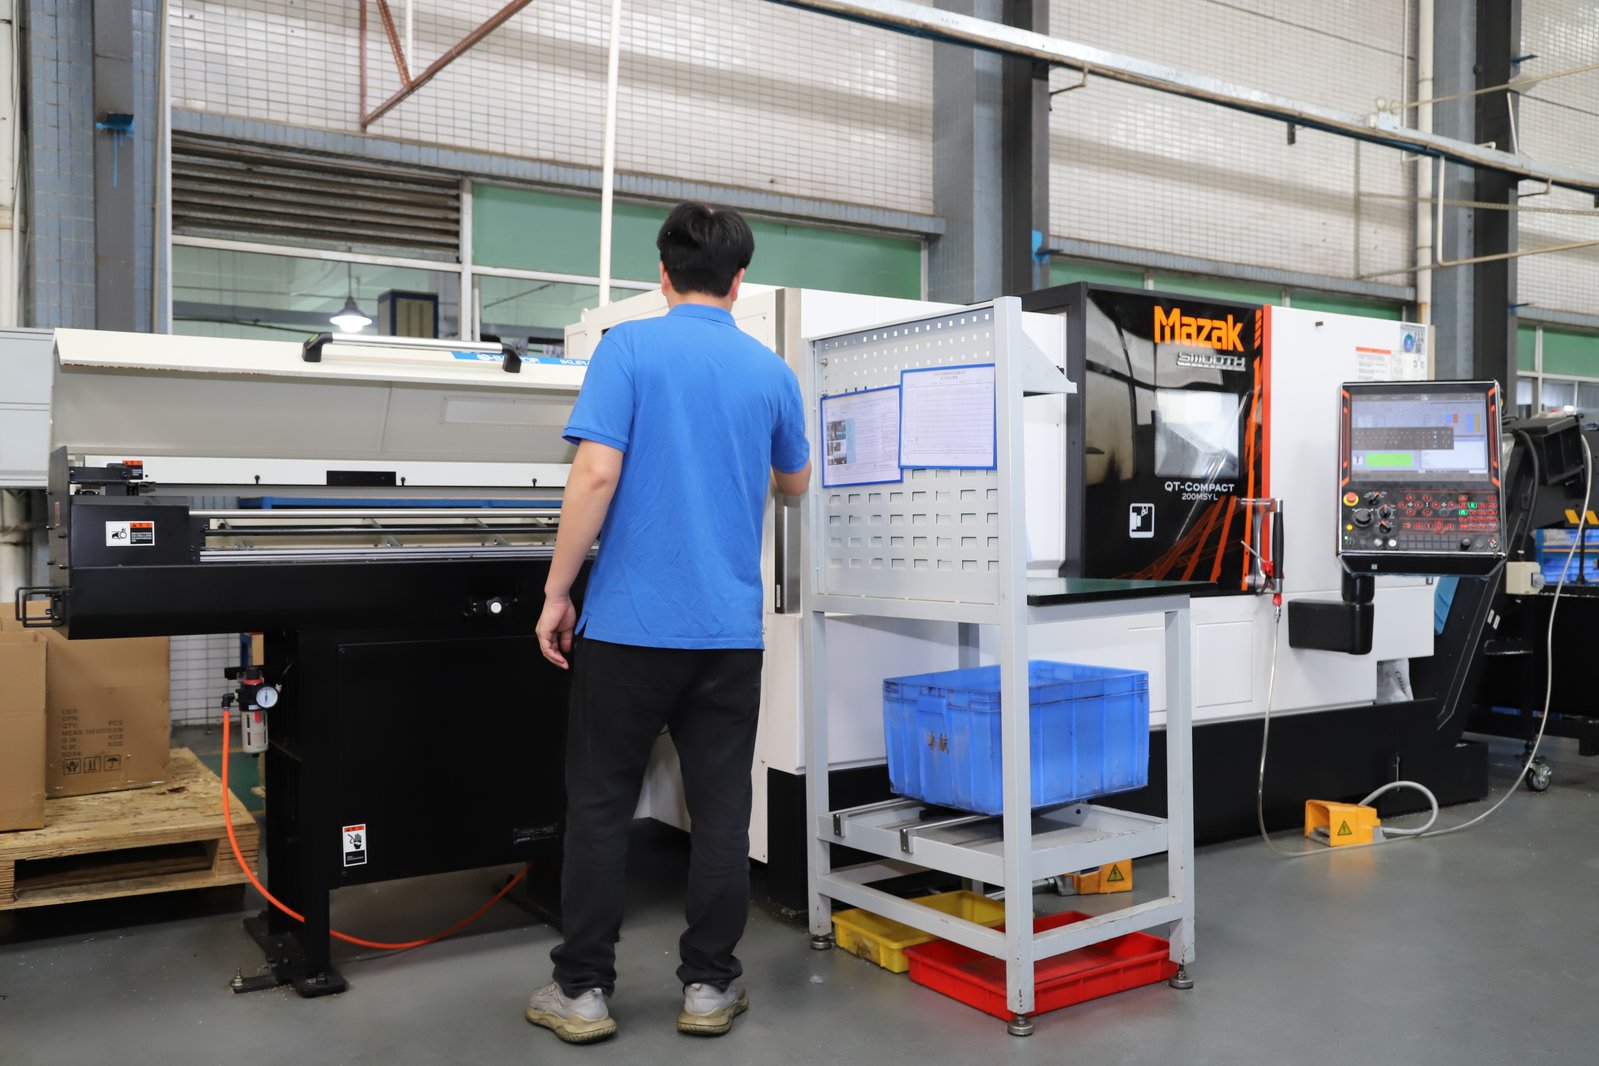
If you ask for capability evidence, you deserve a specific answer. This facility operates 100+ CNC machines across 6,800 m2 in Dongguan, China, staffed by 100+ people. The machines, listed by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Set up for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Set up for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Set up for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Set up for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Set up for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance bands: ±0.003 mm milled, ±0.002 mm turned, ±0.002 mm ground or wire-cut. Capability indices: Ppk >= 1.67 at the initial study; Cpk >= 1.33 ongoing in production.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En) · IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded) · ISO 14001:2015 (116024/B/0001/UK/En), held by Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, since 2005).
Service area: we supply Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, with worldwide delivery from China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Ask the four questions before you commit
Registration number, machine depth, certificate numbers, and a walk of the floor. Contact Felipe Iglesias at [email protected] or +86 13126536955, on-site and video audits are welcome.
Frequently Asked Questions
Do you certify aluminum material?
Yes. Material certificates are supplied with the parts and incoming stock is checked against the mill certificate — composition by XRF, hardness where specified. Traceability is per heat or per batch as the certificate defines it.
Is inspection documentation included in the quote?
It should be stated explicitly. A first-article report is a document someone has to produce, and whether it is a full dimensional report or a sample plan changes both the cost and what you receive.
Does aluminum cost more to machine than aluminium?
Usually yes, and the reason differs by material: for titanium it is cutting speed and tool consumption, for stainless it is cycle time and work-hardening management. The lever that matters most is usually design depth rather than process choice.
How are parts packed for export?
Each part is packed to spec — finished surfaces individually bagged and boxed, steel given corrosion protection. Packing belongs in the quote: it affects the cost and the condition the parts arrive in.
Can I audit the factory before placing an order?
Yes. On-site visits and video audits are welcome at No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470.
Do you sign NDAs before reviewing drawings?
Yes. Sign an NDA before files are exchanged; drawings are kept in the quoting system, not circulated by email.
What happens if the first article does not conform?
In short, The nonconformance is documented and the corrective action is agreed before any further parts are made. Whether the replacement cost sits with the plant or the customer depends on where the deviation came from, which is why the revision and the drawing standard are confirmed in writing at the start.
Continue reading: 3 Axis CNC Turning Service · 4 Axis CNC Turning Service · 5 Axis CNC Turning Service
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM A276/A276M-17 — Standard Specification for Stainless Steel Bars and Shapes
- ISO 9001 — Quality management systems — Requirements