
Most machining disputes are not about the drawing being wrong; they are about the buyer expecting a number the process was never asked to deliver, or a surface the drawing never named. Tolerances and surface finishes are the language that prevents that — the tolerance says how close the part must come to the nominal geometry, the finish says what the surface must look and feel like — and both are only useful when they are stated in measurable terms on the drawing. This guide explains what a CNC turning service can actually hold, what the numbers mean, how tolerance and finish interact, and how to call them out so the quote, the part and the inspection report agree.
What does a tolerance actually mean on a turned part?
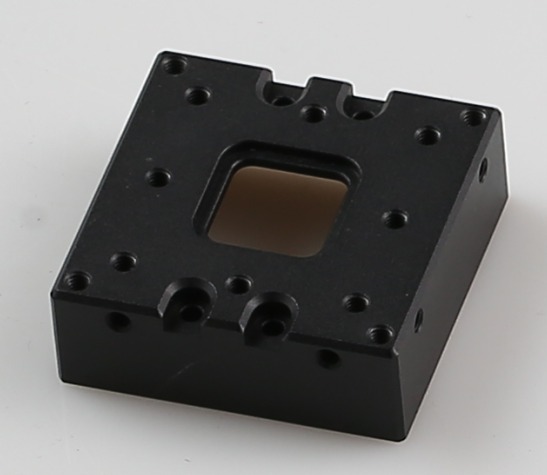
A tolerance is permission: it defines the allowable window around the nominal dimension inside which the feature must fall. A hole called out at 10.00 mm ±0.05 mm must measure between 9.95 and 10.05 mm; the same hole at ±0.002 mm (turning) / ±0.003 mm (milling) must measure between 9.995 and 10.005 mm — a window ten times smaller, which demands a different process and a different inspection method. The tolerance is not a description of what the shop will probably achieve; it is the contract for what the part must be, and it is the number the inspection report verifies.
your responsibility is to set tolerances that match function, because tolerance is cost. Every feature pulled into a tight band adds process care and inspection time, whether the assembly needs it or not. A feature that locates another component, seats a bearing or seals a fluid justifies a tight callout; a cosmetic shoulder or a free surface does not. The discipline is to ask, for every dimension, what happens if this feature is 0.05 mm off, and to tolerance only the features where the answer is "the part does not work."
What can a CNC turning service actually hold?
The capability band a serious CNC turning service should state without hedging is ±0.002 mm (turning) / ±0.003 mm (milling) on machining and ±0.002 mm on precision grinding, with process capability of Ppk ≥ 1.67 at the initial study on key characteristics. The first number is the practical design ceiling for machined features — bores, pockets, datum faces — held on modern machining centers with good fixtures and proper tooling. The second belongs to grinding, which refines surfaces after machining where the part's function demands a tighter size or a finer finish than machining can produce economically.
The words "can hold" carry a process-capability meaning that matters at volume. A supplier can make one part to ±0.002 mm (turning) / ±0.003 mm (milling) by skill and patience; holding it across a production run requires a process that is centered and stable, which is what Ppk ≥ 1.67 initial measures on key characteristics. Ask the supplier which features are treated as key characteristics and how capability is reported, because on a production order the capability number is the honest translation of "we can hold that tolerance", and on a prototype, the honest translation is actual measured values, since capability cannot be measured on a sample of one.
GD&T: position, flatness and parallelism versus blanket ± callouts
A single ± tolerance on a dimension does not fully control a feature. Two holes can each measure within their size tolerance and still be in the wrong place relative to each other; a face can be within its size tolerance and still be bowed. Geometric dimensioning and tolerancing closes that gap by defining what a feature must do — position controls where a hole is relative to its datum, flatness controls how flat a surface is, parallelism controls a surface's relationship to another. On parts with multiple features that must work together, GD&T is not a decoration; it is the only complete description of the requirement.
The buying consequence is that GD&T callouts should appear on the drawing where relationships matter, and the supplier should be expected to verify them as called out — a position tolerance is verified on a CMM against the datum structure, not by a caliper on the hole size. When a drawing relies on blanket ± tolerances for everything, the shop interprets the intent, and the interpretation may not match yours. State the datum structure and the relationships the assembly depends on, and let the general tolerance block cover the dimensions that genuinely do not matter.
Surface finish: what Ra means and what values to expect
Surface finish is usually specified as Ra — the arithmetic average deviation of the surface profile from its mean line, measured in micrometres. Lower is smoother. A rough-sawn or heavily machined surface may sit above Ra 3.2 µm; a standard machined finish typically lands in the Ra 1.6–3.2 µm range; a fine machined finish with light cuts and sharp tooling reaches Ra 0.8 µm and below; and grinding or polishing takes surfaces to Ra 0.4 µm or finer. The numbers are only meaningful with the process and direction behind them, so the drawing should name the value and, where it matters, the method.
your mistake is specifying a finish tighter than the function needs, because every step down the Ra scale costs process time. Ra 3.2 µm is a normal machining finish at no premium; Ra 0.8 µm asks for careful finishing passes; Ra 0.4 µm usually means grinding or polishing, a separate operation. Ask what Ra value the machining process produces on the material you chose — aluminum finishes more readily than stainless, and a "smooth surface" note on the drawing invites three different interpretations and three different prices, while a named Ra value invites one.
| Ra value | Typical process | Typical use |
|---|---|---|
| Ra 1.6–3.2 µm | Standard CNC machining | General machined surfaces, non-critical faces |
| Ra 0.8 µm | Fine machining with finishing passes | Mating faces, visible cosmetic surfaces |
| Ra 0.4 µm | Grinding or polishing | Sealing faces, bearing surfaces, wear paths |
| Ra 0.2 µm and finer | Precision grinding / lapping | High-precision and optical-adjacent surfaces |
How tolerance and surface finish interact
Tolerance and finish are not independent; they pull on the same process. A tight size tolerance and a fine finish on the same feature usually go together, because both are produced by the same careful finishing pass, but a tight tolerance on a surface that will later be coated or heat treated behaves differently — anodize grows a layer and changes the size, so the machining tolerance must anticipate the coating, and the finish under the coating may matter more than the finish on top. The drawing that separates the two requirements — size tolerance here, finish there, coating allowance stated — is a drawing the shop can execute without guessing.
The interaction also runs through the material. Aluminum holds fine finishes readily; austenitic stainless demands controlled speeds and feeds to avoid tearing and work-hardening; and the hard alloys trade away finish for tool life. When a design calls a fine finish on a difficult material, expect the supplier to price the process care and to verify the result with a profilometer rather than a visual check. State both the Ra value and the inspection method where the finish is functional, and the inspection report will carry the number instead of the word "looks fine."
When does a turned part need grinding or another finishing process?
Milling establishes geometry efficiently, but some requirements sit beyond it. A feature called at ±0.002 mm, or a surface needing Ra 0.4 µm or better, is normally ground after machining — the machined feature leaves stock and the grinder refines it to size and finish. Grinding is also the answer for hardened materials that machining cannot cut economically, because grinding cuts hard surfaces that a mill would struggle with. When a drawing carries one of these requirements, the process plan should name the grinding operation and the inspection method, and the supplier's stated band — ±0.002 mm on precision grinding — is the capability it should be held to.
your job is to use grinding only where the function earns it. One ±0.002 mm journal on a shaft or one sealing face at Ra 0.4 µm is a legitimate reason to add grinding; a drawing that calls every surface to the tightest band is asking the shop to grind the whole part, and paying for it. State which features need the grinding band and why, and let the design-for-manufacturing review tell you whether a feature could be reallocated to a machined tolerance at no functional loss — the review is free, and the savings are permanent.
How are tolerance and finish actually measured?
A tolerance is only as credible as the instrument that verifies it. Sizes and positions on turned parts are verified on calibrated instruments — micrometers and calipers for simple sizes, CMMs for position, form and datum relationships, and bore gauges or air gauges for tight internal diameters. Surface finish is measured with a profilometer that traces the surface and reports the Ra value, not by a finger or a "looks smooth." The inspection report should name the instrument for each characteristic, because a ±0.002 mm (turning) / ±0.003 mm (milling) claim verified on a CMM and one verified on a tape measure are different statements.
Ask the supplier which characteristics are inspected 100% and which by sampling, and how the instruments stay calibrated — calibration records are part of the evidence a quality system keeps. On a production lot, SPC data on key characteristics reported against the Ppk ≥ 1.67 initial-study target tells you the process is stable, not just that the sample passed. And set the measurement expectations at the quoting stage: agree which features carry the tight band and which instrument verifies each, so the report that arrives matches the report you expected. On tolerance and finish, the drawing, the process and the inspection method are one system — name all three and the part will measure what the design intended.
Putting the callouts on the drawing so the quote and the part agree
Write the requirement so a stranger can execute it. Name the datum structure and the relationships that matter with GD&T state the tight tolerances on the features that function and leave the rest to a sensible general tolerance block; specify surface finish as an Ra value with the surface it applies to and the method of verification where it is functional; and note any coating or heat-treat allowance that changes the machined size. A drawing that reads this way quotes lower, because the supplier prices certainty instead of guesswork, and it inspects faster, because the report has a checklist that matches the drawing.
Then test the callouts with the quote: ask the supplier to confirm, in writing, the tolerance per critical feature and the instrument that verifies it, and the finish per functional surface and how it is measured. A supplier that answers with numbers and instruments is pricing a part it understands; one that returns a total and a promise is pricing a hope. On the first order, review the dimensional report and the finish readings before release — the actual values will tell you where the process sits relative to the limits, and the design-for-manufacturing notes will tell you which callouts were harder than they needed to be. Tolerance and finish are the cheapest design tools you own; spent deliberately, they make every later order cheaper and every inspection report shorter. And keep the callout list short: every dimension and finish on the drawing is a promise the shop will be held to and a line on the inspection report, so each one should earn its place by changing the part or the price.
Get the callouts reviewed before the part is machined, not after. The design-for-manufacturing review that comes with the quote is the cheapest tolerance consultant you will ever hire — it will tell you which callouts are costing process time for no function, which datum structure makes the part easier to hold, and which finish is finer than the application needs. Send the drawing to more than one supplier and compare the DFM notes; the supplier that questions your tolerances is the supplier that will hold them, because it has understood them.
What this shop actually runs
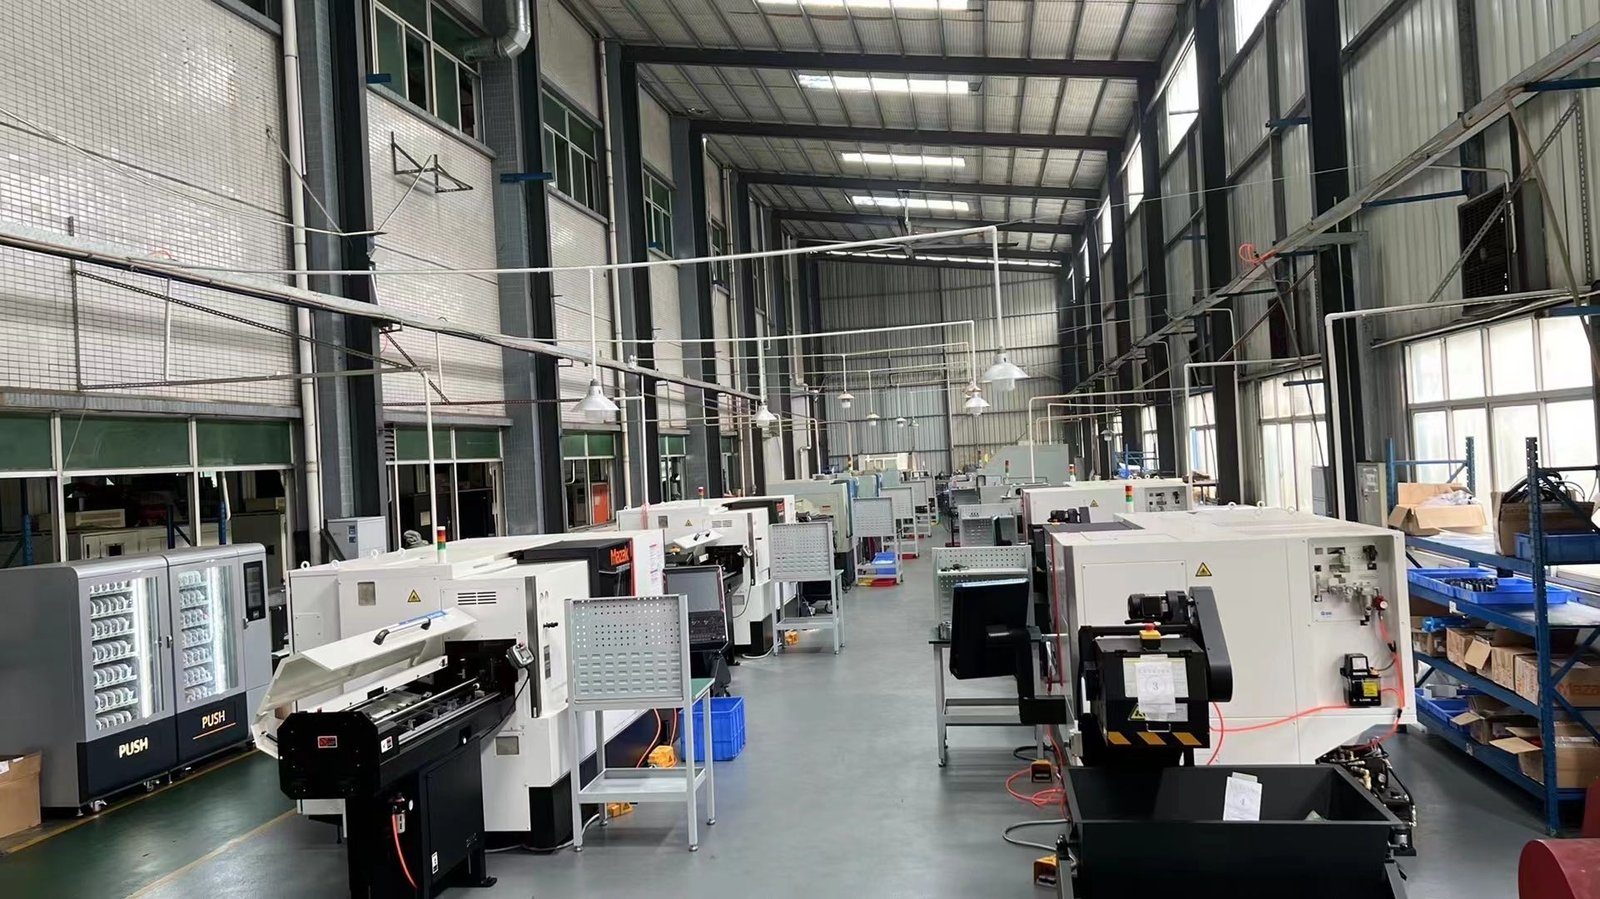
If you ask for capability evidence, you deserve a specific answer. This facility operates 100+ CNC machines across 6,800 m2 in Dongguan, China, staffed by 100+ people. The machines, listed by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Set up for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Set up for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Set up for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Set up for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Set up for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance bands: ±0.003 mm milled, ±0.002 mm turned, ±0.002 mm ground or wire-cut. Capability indices: Ppk >= 1.67 at the initial study; Cpk >= 1.33 ongoing in production.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En) · IATF 16949:2016 (131941/A/0001/SM/En, design clause 8.3 excluded) · ISO 14001:2015 (116024/B/0001/UK/En), held by Dongguan Zhuohang Ltd (USCC 91441900MA4UWT6X39, since 2005).
Service area: we supply Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, with worldwide delivery from China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Setting tolerances and finishes on a turned part and want the callouts confirmed in the quote?
Email the STEP or IGES model with your toleranced 2D drawing to [email protected] or call +86 13126536955. You get the tolerance per critical feature with its instrument, the finish per functional surface with its method, and a design-for-manufacturing review of your callouts. See the quality system page for the inspection framework, and the services overview for the process scope behind the numbers.
Frequently Asked Questions
What tolerance can a CNC turning service actually hold?
In short, ±0.002 mm (turning) / ±0.003 mm (milling) on machining and ±0.002 mm on precision grinding, with process capability of Ppk ≥ 1.67 at the initial study on key characteristics. On a prototype the supplier reports actual measured values; on production the capability number over the run is the honest measure.
What is the standard surface finish from CNC machining?
In short, A standard machined finish typically lands around Ra 1.6–3.2 µm. Fine machining with finishing passes reaches Ra 0.8 µm, and grinding or polishing takes surfaces to Ra 0.4 µm and finer.
Is ±0.002 mm (turning) / ±0.003 mm (milling) the same as a standard tolerance?
In short, No. ±0.002 mm (turning) / ±0.003 mm (milling) is a precision band roughly an order of magnitude tighter than general machining tolerances, and it demands a careful process and CMM-level inspection on the features it applies to.
Do I need GD&T or are ± tolerances enough?
In short, ± tolerances control size but not relationship. If holes must sit in a sensible starting point relative to a datum, or a face must be flat or parallel, GD&T callouts are the only complete description, and they should be verified with the datum structure on a CMM.
How much does a finer surface finish cost?
Every step down the Ra scale adds process time. Ra 3.2 µm is a normal machining finish at no premium; Ra 0.8 µm asks for finishing passes; Ra 0.4 µm usually means grinding or polishing. Name the Ra value so the quote reflects the actual requirement.
When should a feature be ground instead of machined?
In short, When the feature needs ±0.002 mm, a finish at Ra 0.4 µm or better, or the material is too hard to mill economically. Milling leaves stock and grinding refines the feature; the process plan should name the grinding operation and its inspection method.
How should I state finish and tolerance on the drawing?
In short, Name the datum structure, tolerance the features that function with GD&T, specify finish as an Ra value with the method of verification where it is functional, and note any coating or heat-treat allowance. Ask the supplier to confirm the tolerance per feature with its instrument in the quote.
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM A484/A484M-24 — Standard Specification for General Requirements for Stainless Steel Bars, Billets, and Forgings
- ISO 9001 — Quality management systems — Requirements